Edwards RV8 Dual Stage Rotary Vane Vacuum Pump

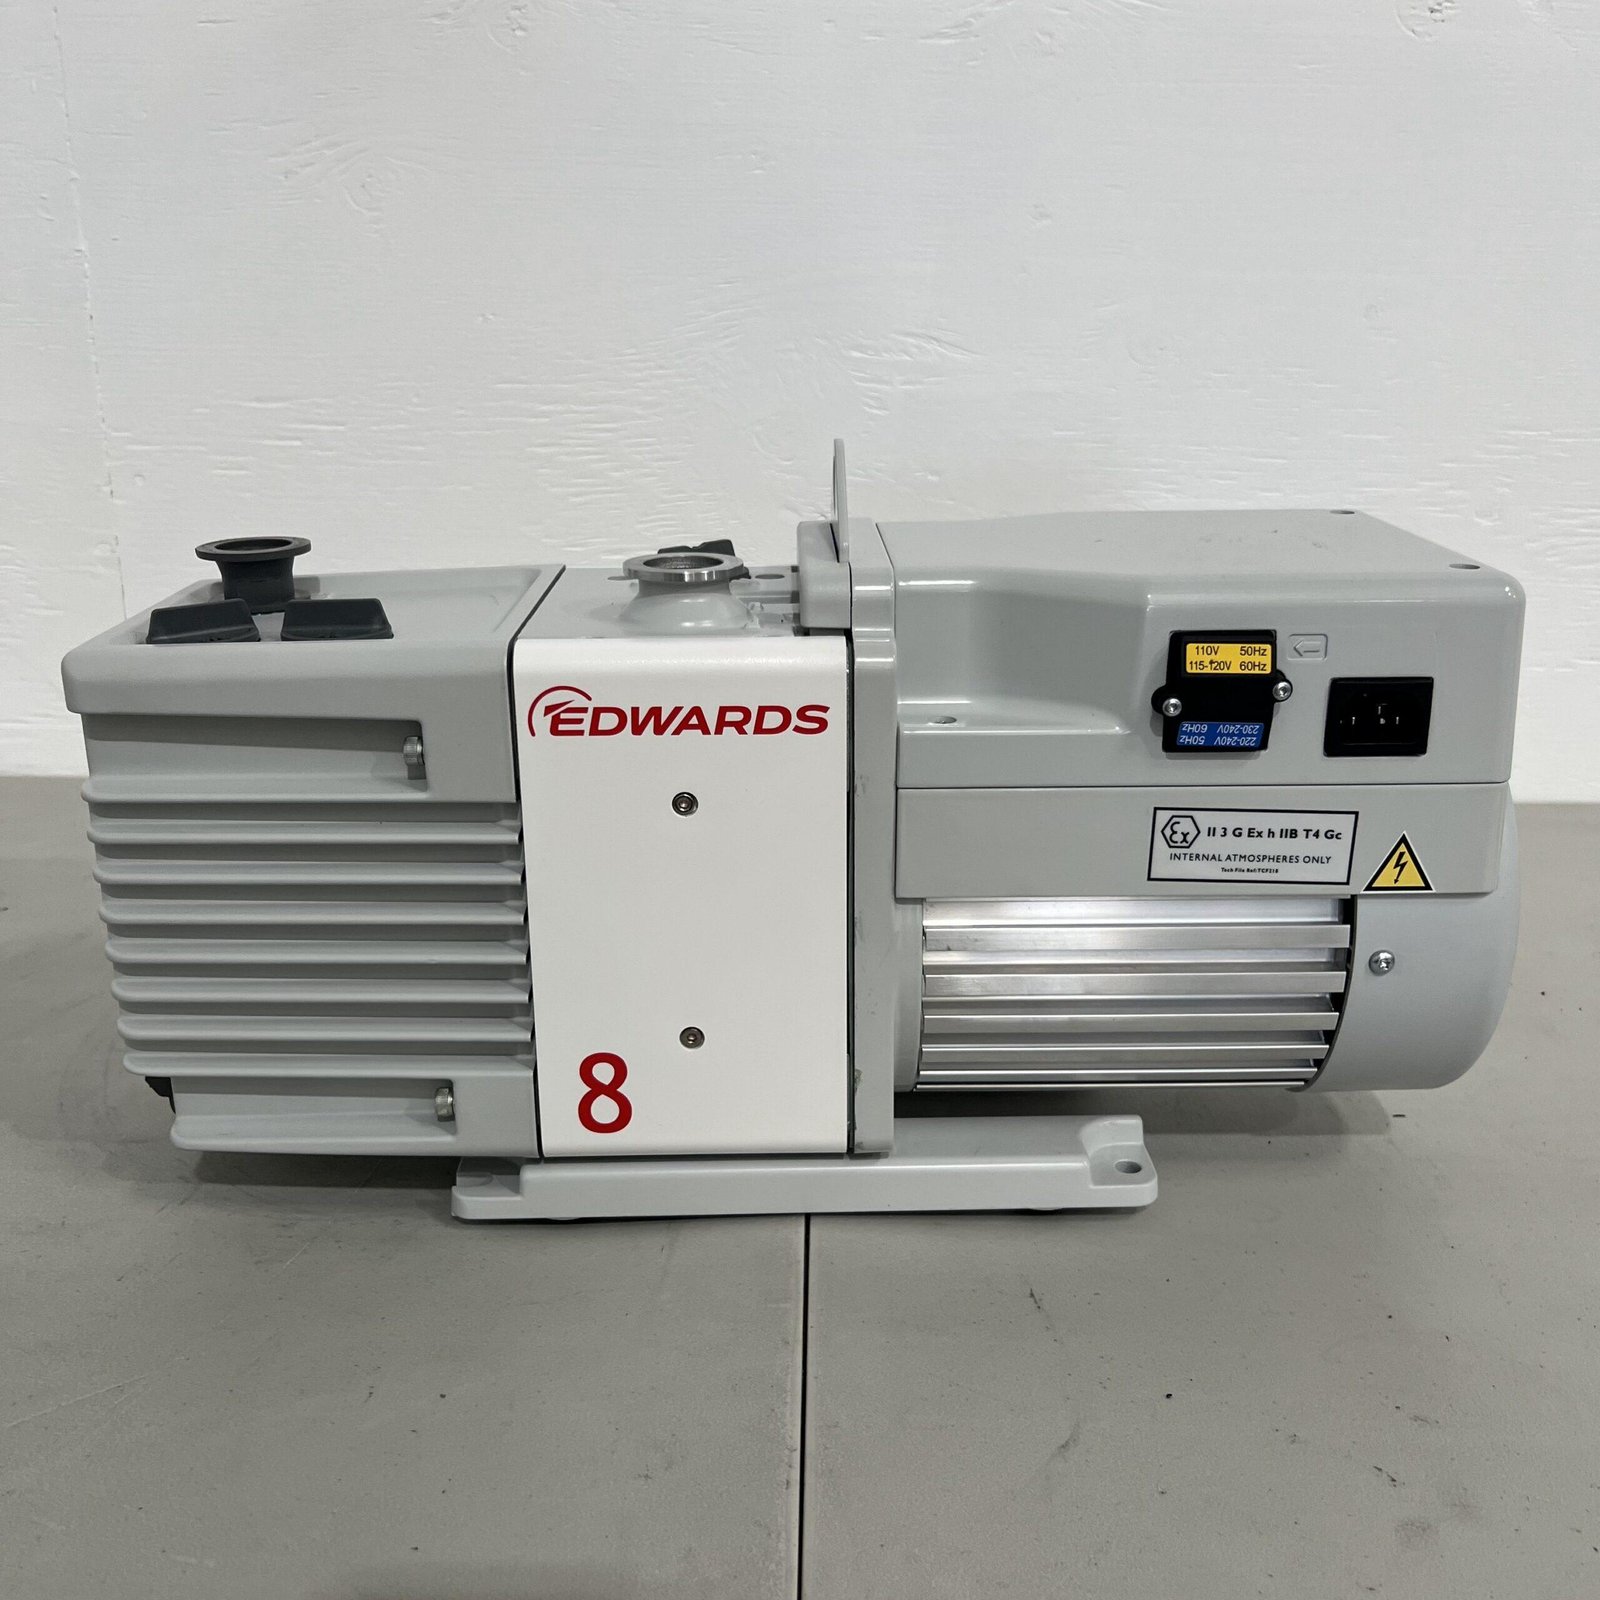
The Edwards RV8 Dual Stage Rotary Vane Mechanical Vacuum Pump (A65401906, 1-Phase) is engineered for demanding laboratory, analytical, and industrial medium-to-high vacuum duties. Designed with a dual-stage rotary mechanism, it provides deep ultimate pressure, strong pumping speeds, and low operating noise. Consequently, research facilities and manufacturing environments can maintain stable process vacuums across continuous shifts.
Key Technical Specifications of the Edwards RV8
- Pump Mechanism: Two-stage, oil-sealed rotary vane configuration
- Displacement Capacity: 9.7 m³/h (5.7 CFM) at 50 Hz; 11.7 m³/h (6.9 CFM) at 60 Hz
- Ultimate Pressure: Down to 2 × 10⁻³ mbar (1.5 × 10⁻³ Torr) in standard high-vacuum mode
- Motor Drive: Single-phase universal motor with integrated dual-voltage selection switch
- Inlet/Exhaust Ports: Standard NW25 (KF25) flanges for quick vacuum line coupling
- Gas Ballast Control: Multi-position gas ballast valve to handle high vapor loads
Core Architecture and Operating Advantages
- Dual-Mode Operation: A distinctive selector allows users to switch between high-vacuum mode and high-throughput mode. As a result, the pump adapts seamlessly to clean analytical tasks requiring maximum base vacuum, or high-gas-load processes needing rapid exhaust evacuation.
- Effective Vapor Purging: The two-position gas ballast selector introduces dry ambient air into the compression chamber. Therefore, condensable vapors such as water or light solvents vent safely through the exhaust without diluting or contaminating the vacuum fluid reservoir.
- Low Noise and Minimal Vibration: Precision-balanced rotating components reduce mechanical resonance significantly. Consequently, the unit runs at approximately 48 dB(A), making it suitable for quiet benchtop operation alongside sensitive laboratory instruments.
- Integrated Suckback Protection: A built-in fast-acting oil suckback valve protects the vacuum chamber. If power disconnects unexpectedly, the valve seals the inlet automatically, preventing oil migration into the connected equipment.
Common Scientific and Industrial Applications
- Analytical Instrumentation: Specifically, it acts as a dependable backing pump for turbomolecular pumps on GC-MS, LC-MS, and residual gas analyzers.
- Vacuum Drying & Freeze Drying: Moreover, it creates the low-pressure atmosphere necessary for freeze-drying cycles, vacuum ovens, and rotary evaporation.
- Centrifugal Concentrators: Additionally, the consistent displacement speeds accelerate solvent evaporation in biotechnology and clinical testing setups.
- Glove Boxes & Schlenk Lines: Consequently, synthesis chemists gain an efficient platform for purging atmospheric moisture and maintaining inert handling conditions.
By pairing adaptable pumping modes with reliable vapor handling, the Edwards RV8 serves as a versatile, low-maintenance workhorse across technical laboratories and pilot production lines.